

Feb 06, 2023
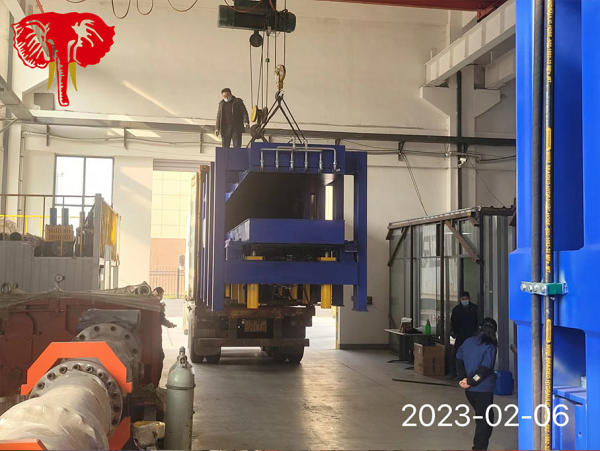
When the shipment is in progress
In February 2023, jinxiang delivered an PU cold room panel press line to a our Nigeria old customer, which is the economic PU line for all initial investors
Read Full Article
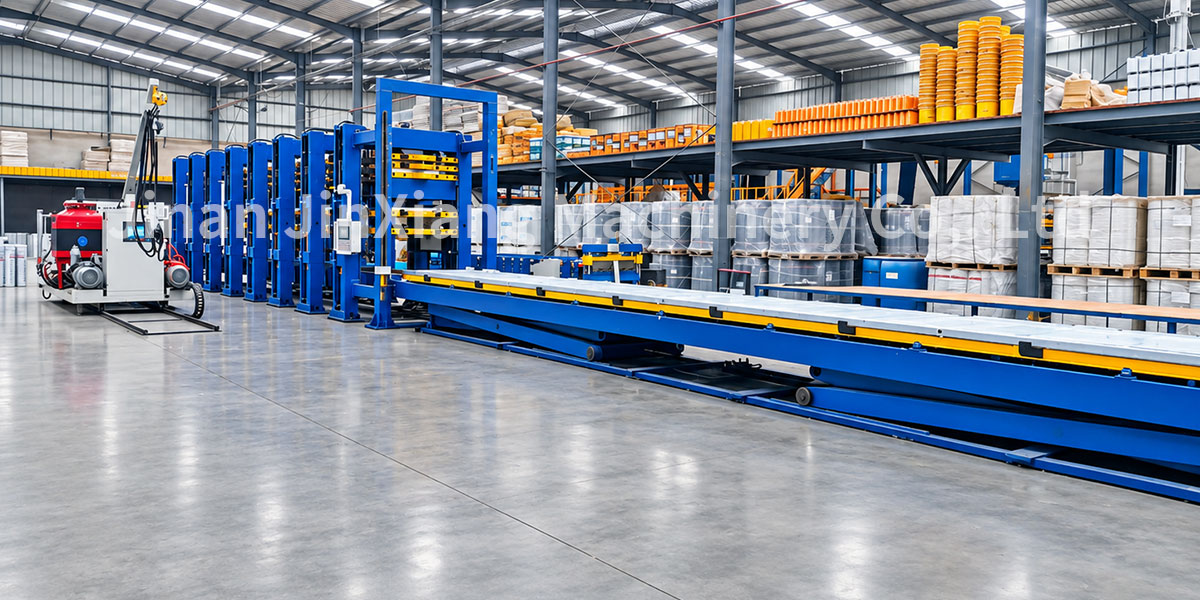
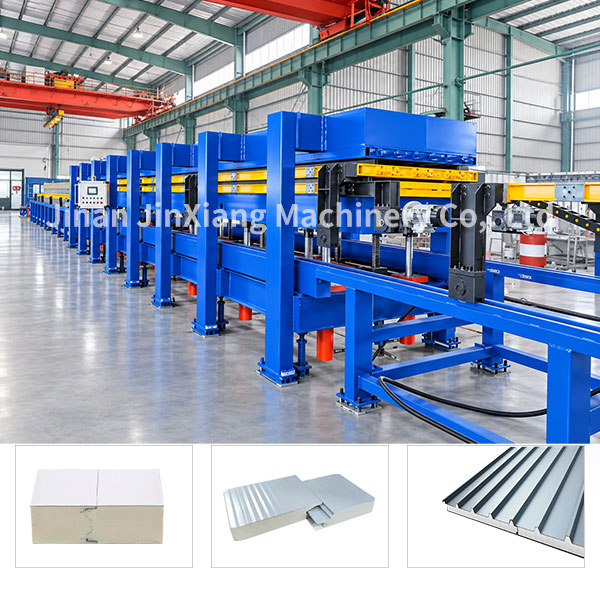
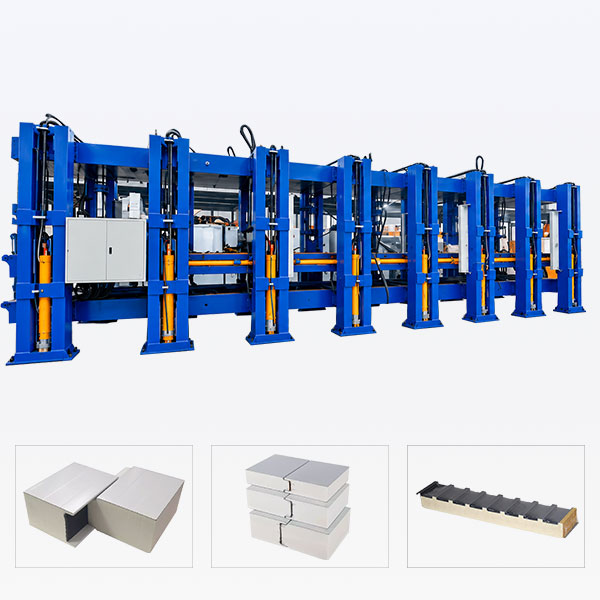
The 3+3 non-continuous PU color steel panel production line (batch PU hot-pressing lamination line) is a polyurethane sandwich panel production equipment adopting an alternating cycle operation mode with 3 stations for pressure holding & curing and 3 stations for loading/unloading & preparation. It is known as the 3+3 hot press line in the industry, mainly customized for cold storage panels, PIR fire-retardant panels, large-size thick panels and special-shaped tongue-and-groove polyurethane color steel sandwich panels. It is an upgraded medium-to-large batch line developed on the basis of the 2+2 model.
Meaning of 3+3: It is equipped with 6 sets of movable mould worktables in total. Three worktables complete material injection, foaming and constant-temperature pressure holding & curing inside the press; the other three synchronously carry out demoulding, panel unloading, color steel sheet laying, tongue-and-groove assembly and edge sealing preparation outside the press. The two groups of stations work in rotation. During the curing cycle, the external preparation stations can finish mould loading for multiple panels adequately, minimizing idle waiting time of the press. Its output is further improved compared with the 2+2 model, suitable for manufacturers with large cold storage panel orders and a high proportion of thick panels.
Different from continuous production lines: It also adopts closed mould injection foaming with independent forming of each single panel. Compared with the 2+2 line, more mould stations can run in parallel. It fits thick panels, extra-long panels, special hook-type tongue-and-groove panels and mixed orders with medium batch quantity & multiple specifications. It can work as the main production line for cold storage panels independently, or cooperate with continuous sandwich panel lines to fulfill orders.
Video Of 3+3 Discontinuous PU sandwich Panel Production Line
Applicable panels:
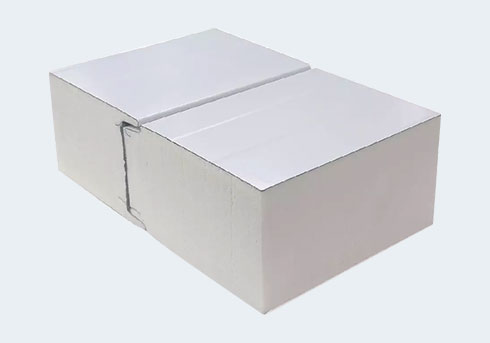
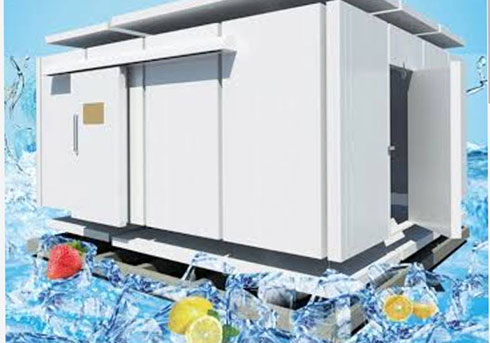
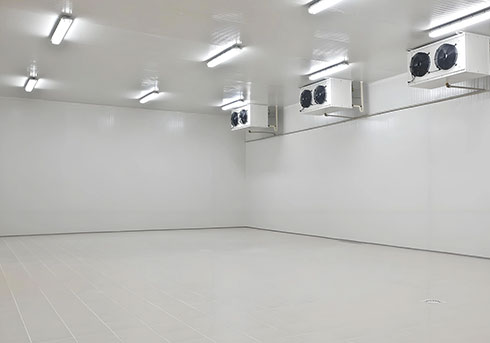
PU / PIR fire-retardant color steel sandwich panels. Face sheets can be galvanized color steel sheets, galvalume sheets, stainless steel sheets or aluminum sheets. Panel thickness ranges from 50 mm to 250 mm, standard width ≤1200 mm, available lengths of 6 m / 9 m / 12 m (customizable for extra length). Widely used in low-temperature quick-freezing cold storage, refrigerated truck bodies, medical constant-temperature warehouses, cleanrooms, constant-temperature workshops, thermal insulation shelters and exported prefabricated cold storage projects.
Main Technical Parameters/Specifications of 3+3 Discontinuous PU sandwich Panel Production Line
Main Components of the Complete Line
1. Uncoiling, color steel forming and shearing system (pre-treatment of color steel face sheets, ribbing, tongue-and-groove forming, fixed-length cutting)
2. Hydraulic hot press main unit (heavy-duty frame, multiple groups of hydraulic cylinders, water-circulation constant-temperature heating platens, long-distance mould guide rails)
3. Six sets of movable mould worktables (equipped with sealing frames, quick-change tongue-and-groove stops, water-circulation constant temperature system)
4. High-pressure PU foaming metering system (compatible with polyol & isocyanate, cyclopentane / HFO eco-friendly blowing agents, closed-loop precise metering)
5. Mobile injection trolley / traversing mixing head (capable of sequential injection for 3 cavities)
6. Temperature control system, hydraulic control system, PLC HMI system (independent formula storage for multi-station)
7. Auxiliary units: vacuum panel lifting fixture, finished panel conveyor, trimming and packing station
Production Process
The whole line adopts a batch closed-loop cyclic process with six mould worktables operating in rotation:
1. Pre-treatment of color steel face sheets
Steel coil uncoiling → roll forming (ribbing and tongue-and-groove forming) → fixed-length cutting. Upper and lower color steel sheets are prepared. Surface cleaning and priming can be applied to improve adhesion between core foam and steel sheets.
2. Mould loading at external stations (3 external worktables work simultaneously)
The worktable moves out of the press. Lay the bottom sheet, install surrounding sealing frames and hook-type tongue-and-groove modules, place side baffles, lay the top color steel sheet, close and seal the mould, and take anti-leakage measures.
3. Worktable exchange into the press
Three loaded worktables are pushed into the hydraulic hot press synchronously. Meanwhile, three fully cured worktables are moved out of the press for station exchange.
4. High-pressure injection and closed foaming
The traversing mixing head extends into the three mould cavities in sequence. Polyol and isocyanate are metered precisely according to the formula, mixed under high pressure and injected into the cavities at a constant speed. PU raw materials foam and expand freely in the confined space to fill the entire panel cavity.
5. Constant-temperature pressure holding & curing (core process)
The hydraulic system clamps the mould and maintains pressure. Heating platens adopt water-circulation constant temperature control (temperature set by formula). Curing time is adjusted according to panel thickness (normally 8–15 min; longer for thicker panels) to ensure foam full maturation, strong bonding and no deformation.
6. Demoulding and panel unloading
After curing, the worktable moves out of the press. Operators open the mould frame with vacuum lifting tools and take out the finished PU color steel sandwich panel.
7. Post-processing, inspection and packing
Panels are cooled, trimmed and cleaned of flash. Random inspection on appearance, dimension and thickness is carried out. Qualified panels are stacked, film-wrapped and packed for storage.
8. Cycle
Empty worktables return to the preparation station for sheet laying and mould loading again to realize continuous cyclic operation.
Supplementary Supply Description
We can supply the 3+3 hot press main unit separately, or provide a complete turnkey solution including uncoiling & forming line, high-pressure foaming system, full set of moulds, hydraulic system, electrical control system, vacuum lifting fixtures and finished panel conveyor line. Customization based on drawings, voltage adaptation, overseas installation guidance and formula commissioning are available.
Samples and Applications
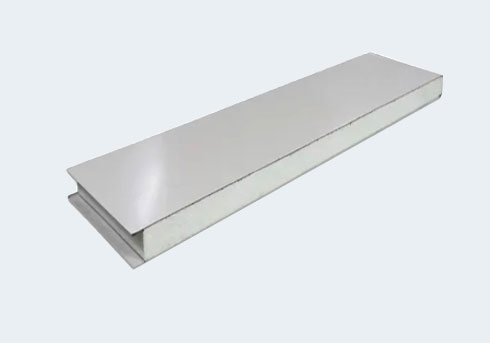
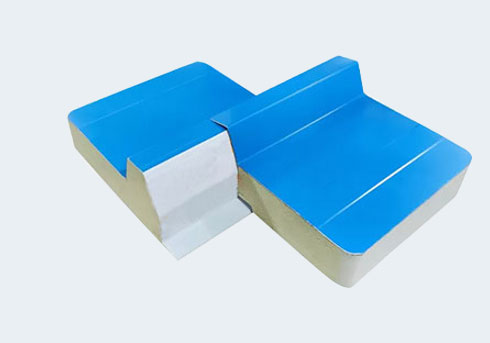
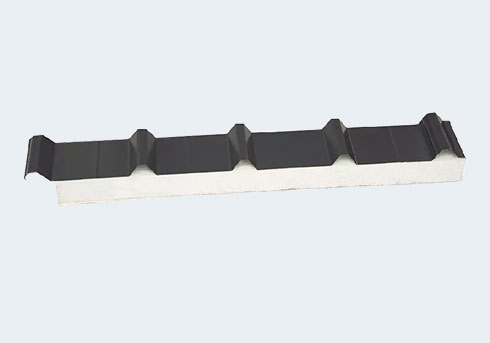
START NOW
Email us with inquiries or use our contact data. We would be happy to answer your questions.
Related Product Recommendations
Latest News & Blog
Feb 06, 2023
In February 2023, jinxiang delivered an PU cold room panel press line to a our Nigeria old customer, which is the economic PU line for all initial investors
Read Full Article
Feb 23, 2023
GET IN TOUCH
Whether you are planning a sandwich panel, XPS foam board, or SIP panel production project, we can provide equipment solutions and technical support tailored to your needs. Complete the form, and our team will be in touch shortly.
* We promise to abide by the confidentiality agreement and strictly protect the relevant privacy content filled in by customers.